Cut resistant gloves for metal and glass must match the level to the edge — a sheet metal edge, a glass pane, and a knife blade each need a different rating and construction, and choosing by the label instead of the task produces the wrong glove. This guide covers the selection logic, with reference to Shield Wings’ cut resistant gloves.
Last updated:
What Do Metal and Glass Tasks Actually Do to Gloves?
Metal and glass tasks combine three stresses — sharp edges, abrasive surfaces, and repeated contact — so the glove must resist cut-through while surviving abrasion and keeping enough dexterity for handling.
A sheet metal edge cuts with pressure; glass edges and fragments cut with sharpness and can shatter under force; wire and fasteners add puncture risk. Handling these materials also drags the glove across abrasive edges, wearing the coating and the knit. The right glove for these tasks balances cut resistance with abrasion resistance, grip, and dexterity — a glove that is cut-rated but loses its coating in a week is not protecting anyone. Start by naming the material, the edge, and the contact pattern of each task.
Which Cut Level Do Metal and Glass Jobs Need?
Light handling of smooth sheet edges needs ANSI A2–A4; cutting, blanking, and glass handling need A4–A6; and heavy fabrication with sharp tooling needs A6–A7 or higher — with the straight-blade rating as the guide.
| Task | Recommended level (ANSI/ISEA 105) |
|---|---|
| Light sheet handling, packaging | A2–A3 |
| Metal cutting, glass handling | A4–A5 |
| Heavy fabrication, sharp tooling | A6–A7 |
| Extreme blade and glass breakage | A8–A9 |
The straight-blade (TDM) rating is the relevant number for these hazards, because it measures force against a sharp edge. Check the full code too: abrasion matters on rough edges, and puncture matters where wire and fasteners are present. When in doubt, test the candidate glove on the actual task before scaling, because real edges vary more than any chart.
What Materials Work for Metal and Glass Handling?
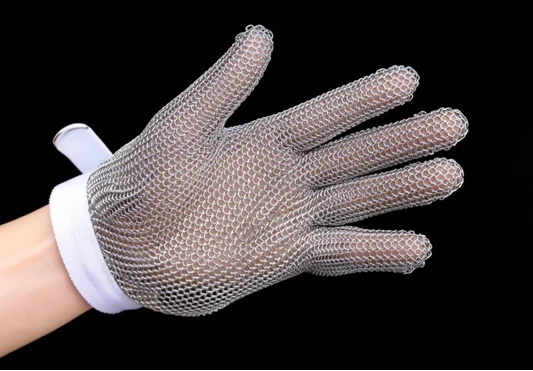
High-performance polyethylene (HPPE) delivers high cut resistance with a light feel, aramid adds heat and strength, and steel mesh or high-denier constructions handle the most extreme blades — each combined with a coating for grip and wear.
HPPE is the workhorse for general metal and glass work, offering strong cut resistance without the weight that destroys dexterity. Aramid blends add strength where edges are aggressive. For the most extreme glass and knife work, steel mesh or very high-denier HPPE constructions are used, accepting the trade-off in comfort and flexibility. The coating — nitrile for grip and oil resistance, polyurethane for precision feel — protects the knit and extends life, and the right coating often matters as much as the cut level.
What Coating Choices Fit Metal and Glass Work?
The coating decides grip and wear: smooth nitrile grips oily sheet metal, foam nitrile channels water on wet glass, and polyurethane preserves dexterity for precise handling — with the coating chosen to match the surface, not the catalog.
Oily and coated metal edges are where grip failures cause dropped parts and cut hands, so a nitrile palm that bites into the surface is the right start. Wet glass calls for foam nitrile, which wicks moisture away from the contact point. Polyurethane is thin and flexible, suiting work that needs fine finger control. Sand-coated or textured palms add grip on smooth, dry surfaces. The coating also protects the knit from abrasion, which is the difference between a glove that lasts a month and one that lasts a season — factor coating wear into the replacement cycle and compare total cost, not just the purchase price.
What About Grip, Fit, and Comfort?
Fit and grip decide whether the glove is worn: a snug fit preserves dexterity for handling, and the right coating keeps a firm grip on oily or smooth surfaces — because a glove that slips or feels clumsy gets taken off.
Glass and metal handling is precise work: aligning edges, lifting panes, and guiding parts require finger feel. Choose the size by palm measurement and test at the end of a shift when hands are largest. Nitrile-coated palms grip oily sheet metal; foam nitrile channels water on wet glass; textured coatings improve grip on smooth surfaces. If the glove is uncomfortable or restricts movement, workers will remove it at exactly the moment the edge is sharpest — so fit and comfort are part of the safety decision, not an afterthought.
Sizing is worth measuring, not guessing: measure the palm circumference of the dominant hand, order samples across the range, and test them through a real task. A glove that fits at the bench may bind once the worker grips a heavy pane, and a glove that feels loose at the palm reduces control of the edge. Keep a fitting station with the approved sizes at the workstation, and let workers swap sizes until the fit is right — the cost of a few extra pairs is trivial next to the cost of a glove discarded mid-task.
How Do You Choose the Right Glove Step by Step?
Work through five steps: name the task and edge, set the cut and abrasion levels, choose the fiber and coating, size and trial the gloves, then verify the test report before bulk ordering.
First, describe the material and how it is handled. Second, write the minimum cut level and any abrasion or puncture requirements. Third, match the construction — HPPE for general work, aramid for heat, higher densities for extreme edges — and the coating to the grip and environment. Fourth, order samples in the sizes your crew needs and trial them on the real task for a shift or more. Fifth, request the test report for the exact model and confirm the delivered batch matches. A sample that performs on the real task, with the report to back it, is the glove to scale.
Cut ratings do not cover puncture, crush, thermal, chemical, or machine-entanglement risks; assess the full task and confirm with the manufacturer’s instructions and the applicable standard.
A Wear Trial That Produces Numbers
Metal and glass handling is where glove choice is most often decided by opinion, because the difference between two candidate levels shows up as comfort rather than as a cut. A short trial with recorded outcomes converts that argument into data the store can act on.
| Trial step | What you record | What it decides |
|---|---|---|
| Two candidate gloves per task | Level, coating and size for each | That the comparison is between named models, not between sales claims |
| Two weeks on the real task | Cuts, near-misses and any glove removed mid-task | Whether the level is right or the glove is being taken off |
| Grip under real conditions | Oily, wet and dry handling notes per candidate | Coating choice, which decides the outcome more often than the cut level |
| Glove life | Pairs consumed per candidate per task group | The replacement line in the budget |
| Worker verdict | Which glove the crew asks for at the end | Whether the specification will actually be worn |
Worked example: a 40-person sheet-metal and glass shop
Illustrative plan. Three task groups — light sheet handling, guillotine and glass handling, and a bench where cut-offs are handled by hand — with two candidate gloves for the two heavier groups. Ten workers per group take part, two pairs each, which is sixty pairs for the trial; the light-handling group keeps its current glove as the control. Two weeks later the store has, for each group, the number of cuts, the number of pairs worn out, and a note on grip in oily conditions. That is enough to set one specification per group and to justify the price difference, or to reject the more expensive candidate with evidence.
Where the cut level stops deciding
Cut level does not predict puncture, and it says nothing about grip: two gloves at the same level behave differently on oily glass, which is why coating appears in the trial table. A high level also costs dexterity, and a glove that gets removed for the fiddly part of the task protects nothing during it. And the rating belongs to the model as tested — change the liner or the coating and you are trialling a different glove, even if the catalogue picture looks the same.
Which Cut Resistant Glove Questions Do Buyers Ask Most?
Do we need the highest cut level for glass handling?
Not always. Match the level to the task — A4–A5 covers most glass handling, while extreme breakage and knife work need more.
Can the same glove cover metal and glass tasks?
Often yes, if the levels and coating suit both. Confirm with a task map and a wear trial before standardizing one glove.
How do we know the rating is real?
Request the EN 388 or ANSI/ISEA 105 test report for the exact model and production, and compare the levels to your task spec.
How do we get samples for a wear trial?
Send us your task list, and we will recommend levels and coatings with samples via our contact page or the cut resistant gloves page.
For the wider topic and related decisions, see our Hand, Cut & Impact Protection.